


coolEX® LM combines DIAHON coolEX honing technology with hydraulic tool expansion and pneumatic diameter measurement using the DPMS 3.0 air gauging system. This allows the honing process to be controlled directly on the machining centre based on the actual measured bore diameter.
The system is designed for very tight finished tolerances. Within the coolEX family, coolEX® LM provides dimensional control < 3 µm, allows larger machining allowances and can handle processes with greater variation in pre-machining stock.
The honing stones are expanded by coolant pressure supplied through the spindle internal coolant system. Machining uses classic honing kinematics with rotation and axial reciprocation and produces a true cross-hatch surface.
With coolEX® LM, the tool function is combined with pneumatic diameter measurement. The measurement signal is made available to the process for finished-size control.
The DPMS 3.0 air gauging system can provide pre- and post-process measurement as well as in-process measurement. This enables micrometre-level monitoring of the bore diameter during the machining sequence and allows the honing process to react to the actual workpiece condition.
Cylindricity deviations can also be corrected by selectively adapting the stroke position of the coolEX® LM tool. The measurement can additionally support 100% quality inspection, documentation and monitoring of defined minimum material removal.
For coolEX® LM, the machining centre is upgraded with the DPMS 3.0 air gauging system and a machine-specific measuring-air transfer. Coolant is routed through the spindle for hydraulic tool expansion, while the measuring air must also be transferred reliably to the measuring nozzle in the tool.
Depending on the machine, the air transfer can be implemented at the spindle nose, at the tool holder or by means of a rotary distributor on the tool. The image examples include an integration on a GROB G350 and a combined air/torque support for HELLER HSK-A63.
coolEX® LM is particularly useful when a bore has to be finished directly on the machining centre to a very tight size and the allowance from pre-machining is not sufficiently consistent. The technology is intended for precision bores where diameter, form and process reliability have to be controlled as one system.
A machine upgrade with the DPMS 3.0 air gauging system is required, together with a suitable design of the tool, measuring-air transfer, coolant supply and CNC process.
| System | Main focus | Dimensional control / process |
|---|---|---|
| coolEX | final surface and cross-hatch | finished size relative to pre-machining; short cycle times |
| coolEXact | defined size control using a stop | < 10 µm; larger allowance possible, allowance should not vary significantly |
| coolEX® LM | closed-loop precision honing with air gauging | < 3 µm; larger and more variable allowance possible; DPMS 3.0 air gauging system required |
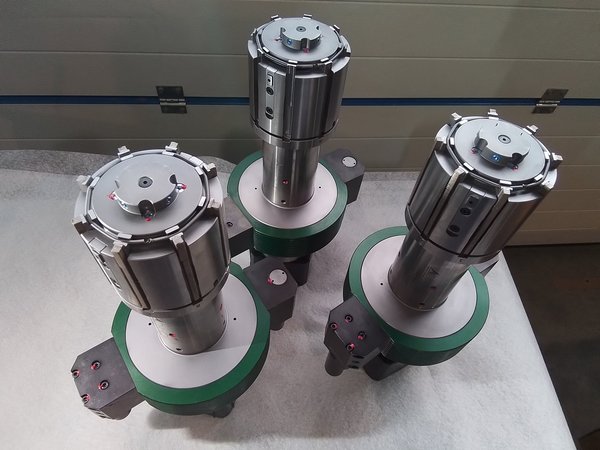
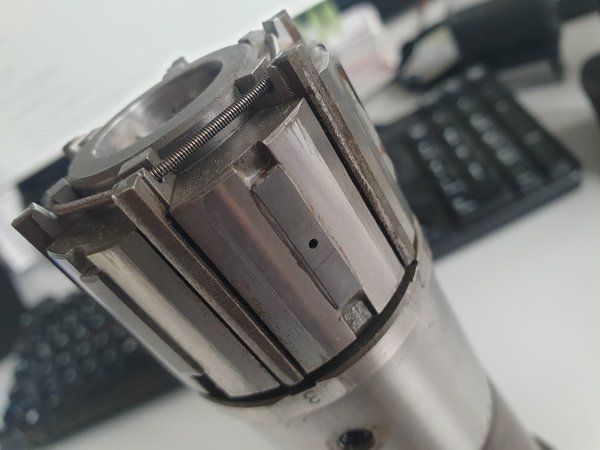
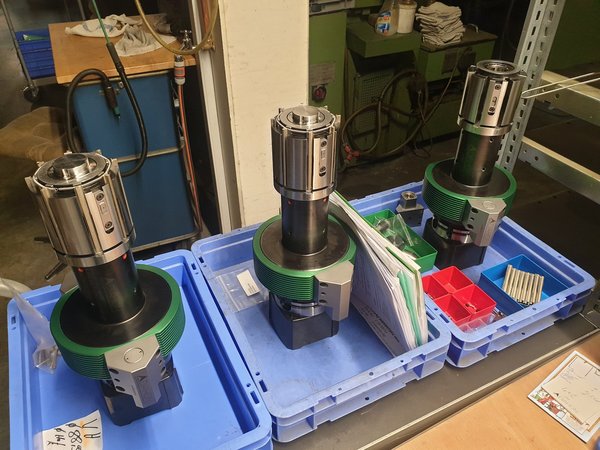
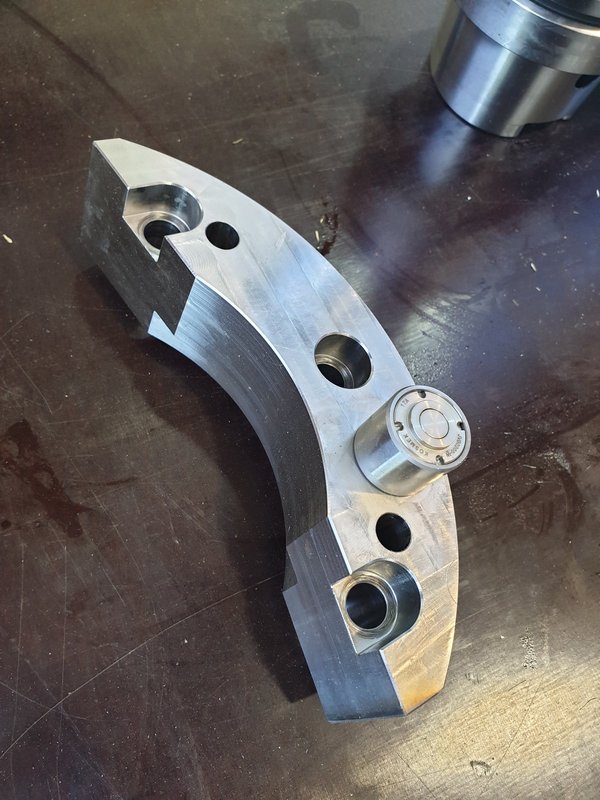
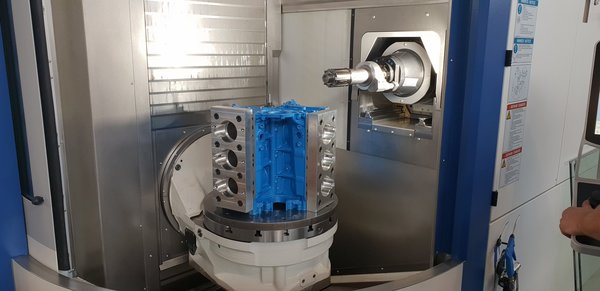
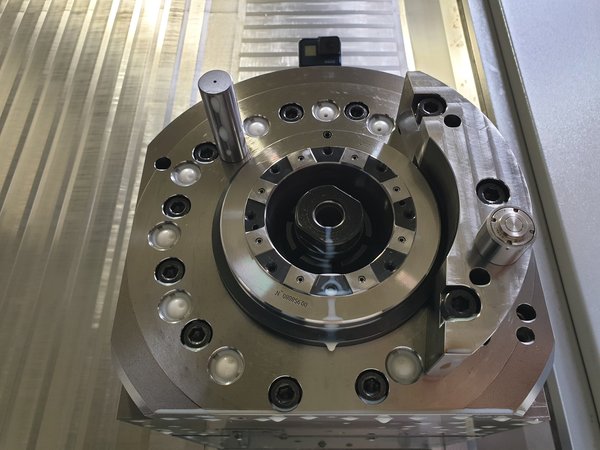
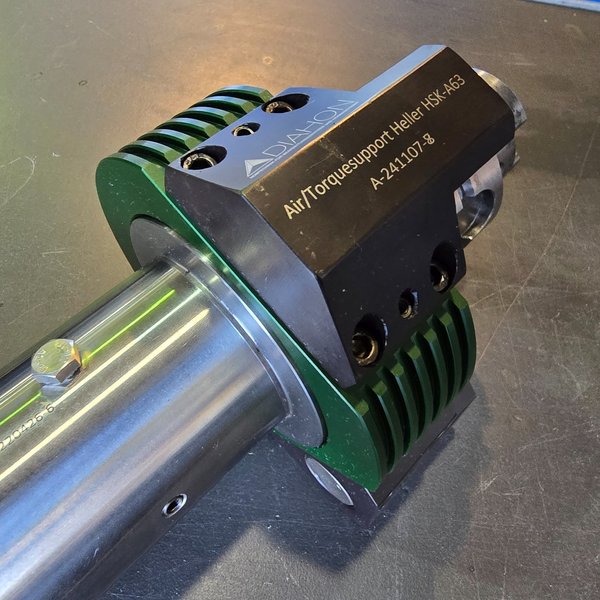
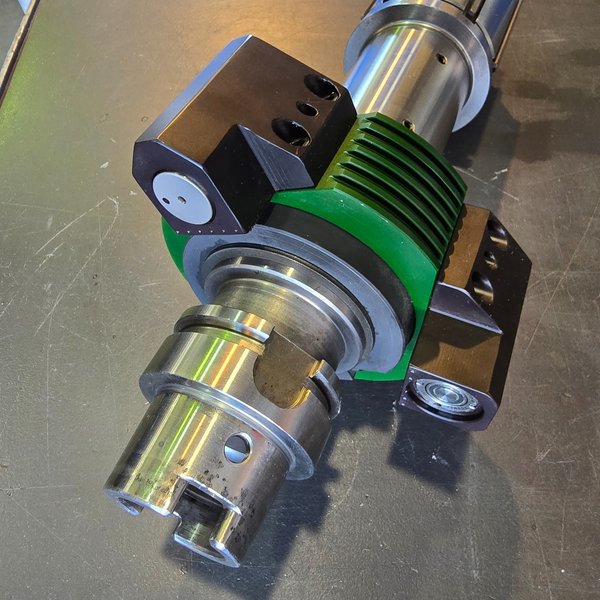
The images show current coolEX® LM tools, the integrated measuring nozzle, different solutions for measuring-air transfer and realised machine integrations on GROB and HELLER machining centres.