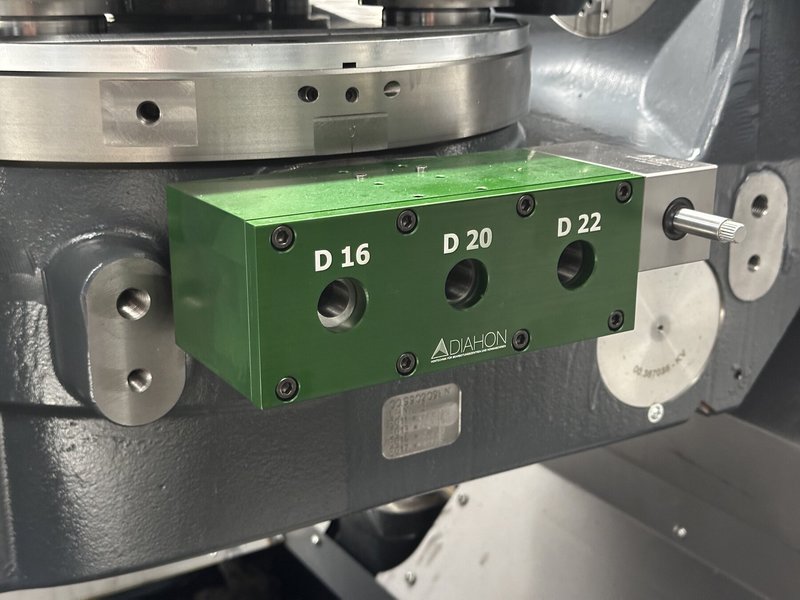
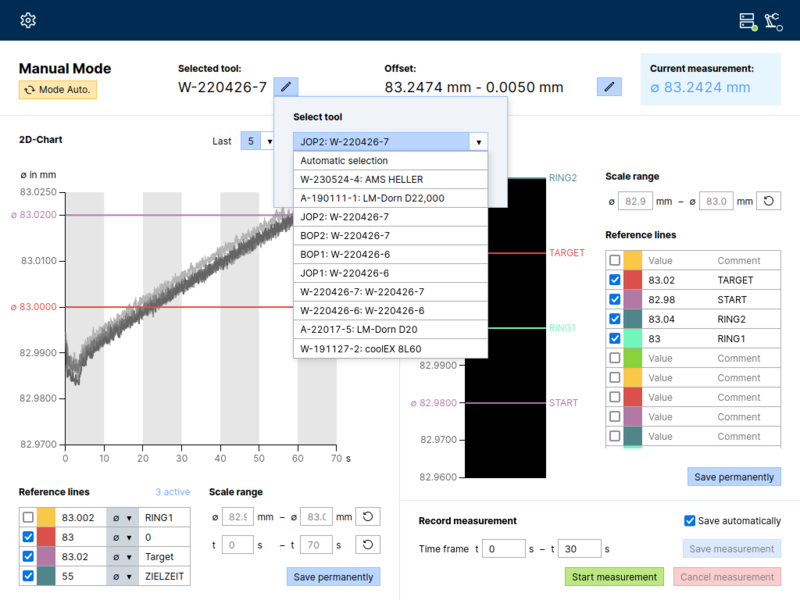
DPMS 3.0 is the DIAHON air gauging system for high-precision pneumatic diameter measurement. The system covers applications ranging from manual single measurements with a handheld air gauge to measurement and control tasks fully integrated into a CNC machine.
Depending on the application, measurements can be taken before, during or after machining. The three versions Light, Eco and Pro differ primarily in tool and calibration-data management and in the degree of machine integration.
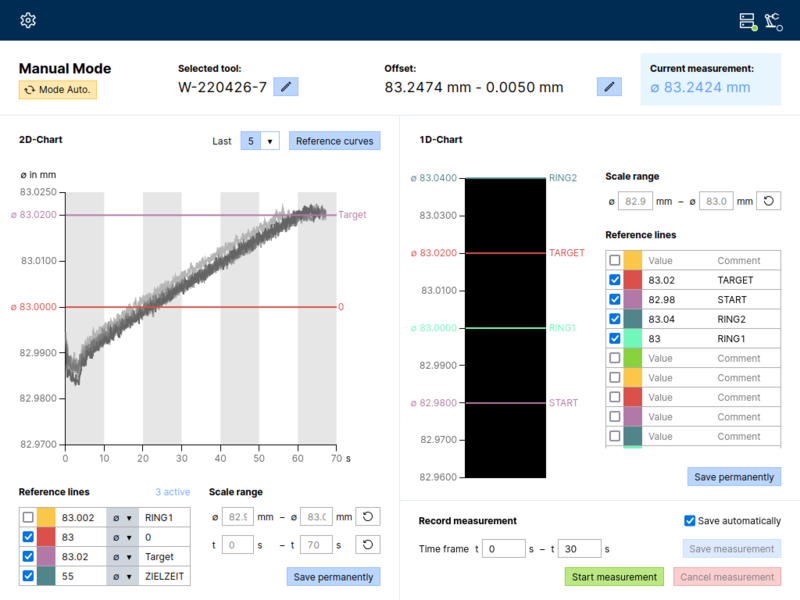
For handheld measurements, all three versions provide two measurement modes:
The Pro version additionally provides a machine-controlled mode. The CNC or PLC commands the start and stop of the measurement.
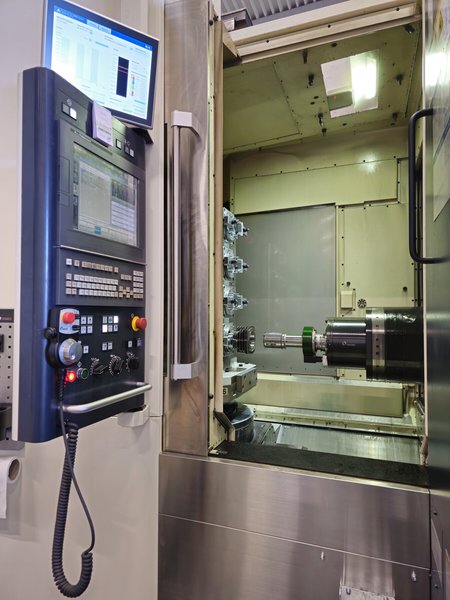
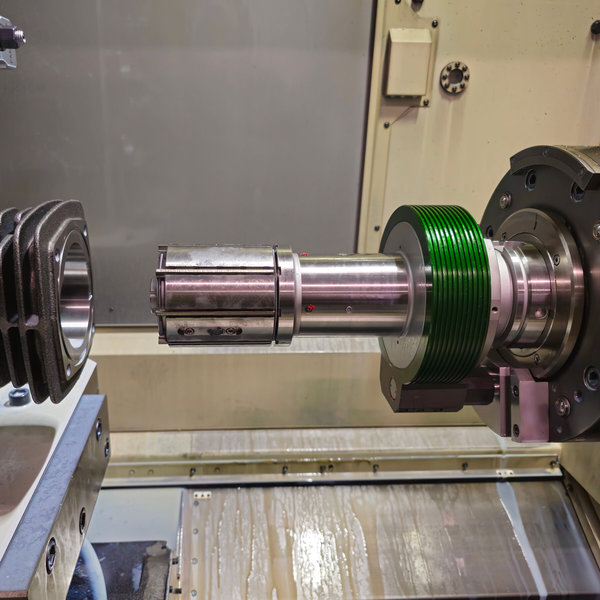
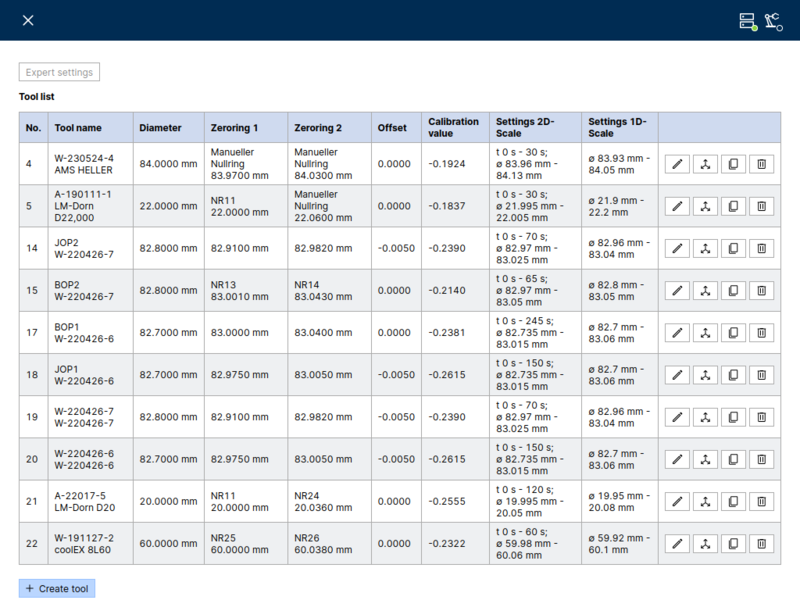
DPMS 3.0 Pro can manage different air gauge mandrels (LMD) and use them for measurements directly in the machine tool. Bores can therefore be measured before machining, inspected after machining or - with a suitable process and tool concept - monitored during machining.
After the machine-side measurement start, DPMS 3.0 Pro continuously transfers the current diameter value to the CNC control. The machine can use this value directly for the subsequent machining process. In addition to honing, possible applications include roller burnishing, reaming and fine boring.
Process parameters can therefore be adjusted according to the measured diameter, or machining steps can be controlled or stopped based on the measurement result. In combination with suitable adjustable DIAHON tools, a closed control loop for diameter control and wear compensation can be implemented.
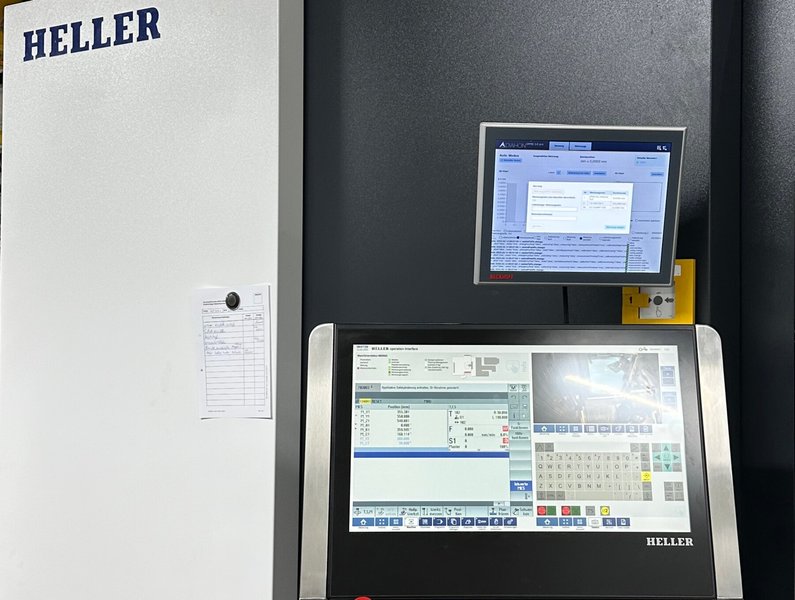
The Pro version connects DPMS directly to the machine control. Depending on the project, communication with the PLC or CNC is implemented, for example, via PROFIBUS, PROFINET or CC-Link.
The machine tells DPMS which measuring or machining tool is currently in the spindle. DPMS therefore automatically identifies the active tool or air gauge mandrel (LMD) and retrieves the stored calibration data associated with it. At the same time, in automatic measurement mode, the machine control provides the signals for starting the measurement and stopping the measurement.
By using different LMDs, different bore diameters can be inspected automatically. Measurement can be integrated into the machine sequence as pre-measurement, post-measurement or - depending on the application - in-process measurement.
The tool database and calibration-ring database are the main confirmed differences between Light and the Eco/Pro versions.
Light does not provide a tool database or a calibration-ring database. Different air gauge mandrels can nevertheless be used; they are simply not managed through these databases.
Eco provides a tool database and a calibration-ring database. This allows multiple air gauge mandrels and their associated calibration data to be managed efficiently.
Pro provides the same databases and adds the CNC/machine interface. This allows measurement sequences and the use of measurement data to be integrated into the automated machine process.
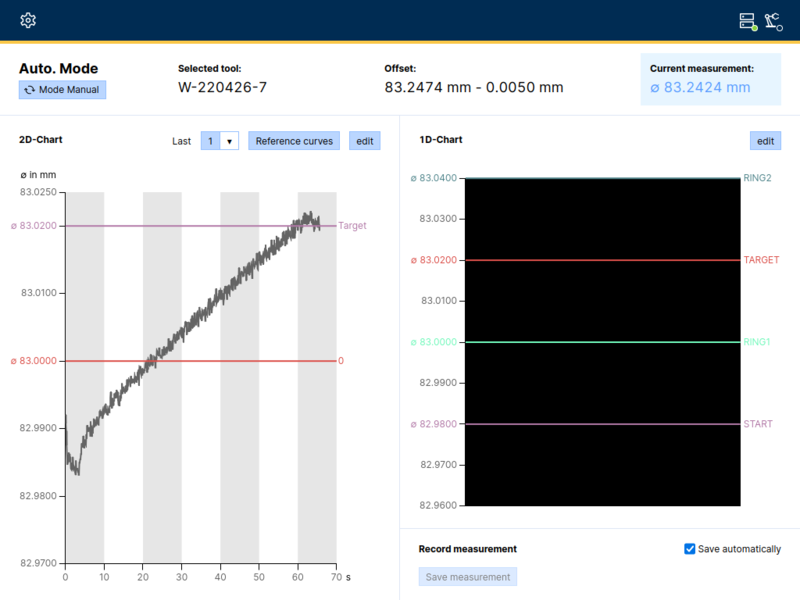
DPMS 3.0 visualises current measured values and measurement histories, making diameter trends immediately transparent. Depending on the version and application, measurements can be documented manually or used within the automated machine process for process and quality monitoring.
In the Pro version, the diameter values are additionally available directly to the CNC through the machine connection.
DPMS installations are used in series production worldwide on machines from various manufacturers, including platforms from MAKINO, COMAU, HELLER, DMG MORI, GROB and STARRAG HECKERT.
The specific configuration is matched to the machine, component, measuring task and required level of automation. Talk to DIAHON about the right integration for your bore machining process.
| Function | Light | Eco | Pro |
|---|---|---|---|
| Evaluation of handheld air gauges | ✓ | ✓ | ✓ |
| Evaluation of boreINspector | ✓ | ✓ | ✓ |
| Tool database | – | ✓ | ✓ |
| Calibration-ring database | – | ✓ | ✓ |
| Database-supported management of multiple air gauge mandrels (LMD) | – | ✓ | ✓ |
| CNC/machine interface | – | – | ✓ |
| CNC-controlled in-process measurement | – | – | ✓ |
| Automated pre-/post-measurement | – | – | ✓ |
| Tool-diameter compensation | – | – | ✓ |
DPMS 3.0 Light operates without a tool database and without a calibration-ring database.
DPMS 3.0 Eco provides a tool database and a calibration-ring database. This allows multiple air gauge mandrels and their associated calibration data to be managed efficiently.
DPMS 3.0 Pro also provides the tool and calibration-ring databases and adds the interface to the CNC/machine control. DPMS 3.0 Pro can therefore be used for in-process measurements as well as for pre-/post-measurements directly in the machine. The measured values can be used for tool-diameter compensation and - depending on the relevant machine and tool concept - for automated process control.
DPMS 3.0 Pro can be operated with different air gauge mandrels (LMD). In addition to honing, possible applications include roller burnishing, reaming and fine boring.
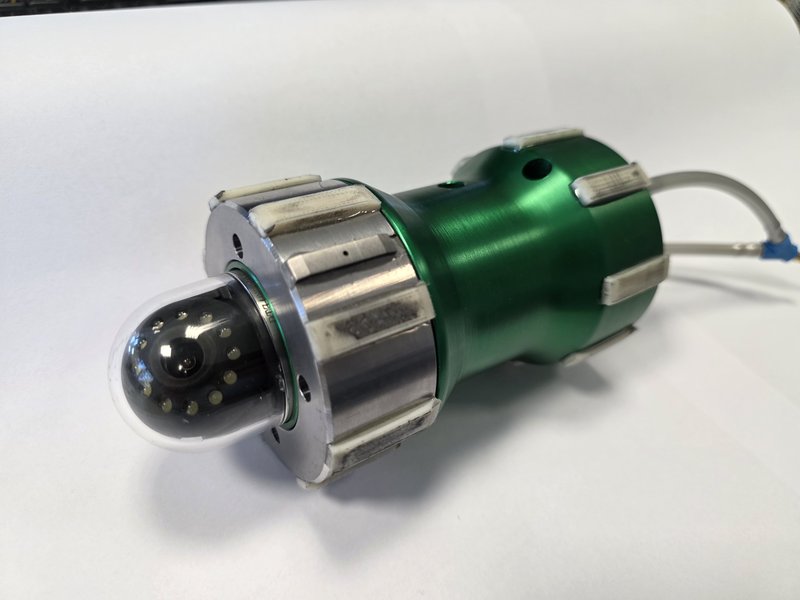
The boreINspector combines the proven high-precision DPMS 3.0 Air gauging system with a dedicated bore-inspection camera. This makes it possible to pneumatically measure the diameter of long bores of less than 15 m over their full depth while visually inspecting them for surface defects.
The solution originated from machining very long bores with DIAHON tools. With conventional inspection methods, often only the end sections of the bore were accessible. Defects inside the bore - such as scratches, steps or bright areas caused by deformation, clamping conditions or other process influences - could therefore only be detected later.
With the boreINspector, the air gauge mandrel and camera head are mounted together on a sliding probe adapted to the bore diameter. A winch unit moves the probe through the bore using a push/pull cable. Diameter variations can first be located with the air gauging system, after which the relevant position can be examined specifically with the camera. Dimensional compliance can therefore be documented over the entire bore depth.
The base unit and winch system can be positioned directly at the machine tool. The component does not have to be unclamped for inspection and can be reworked immediately if required. The system has already been tested; the probe design and further details can be adapted to customer-specific requirements.
The boreINspector therefore combines micron-accurate dimensional diameter inspection and visual surface inspection in one system - directly on long bores.